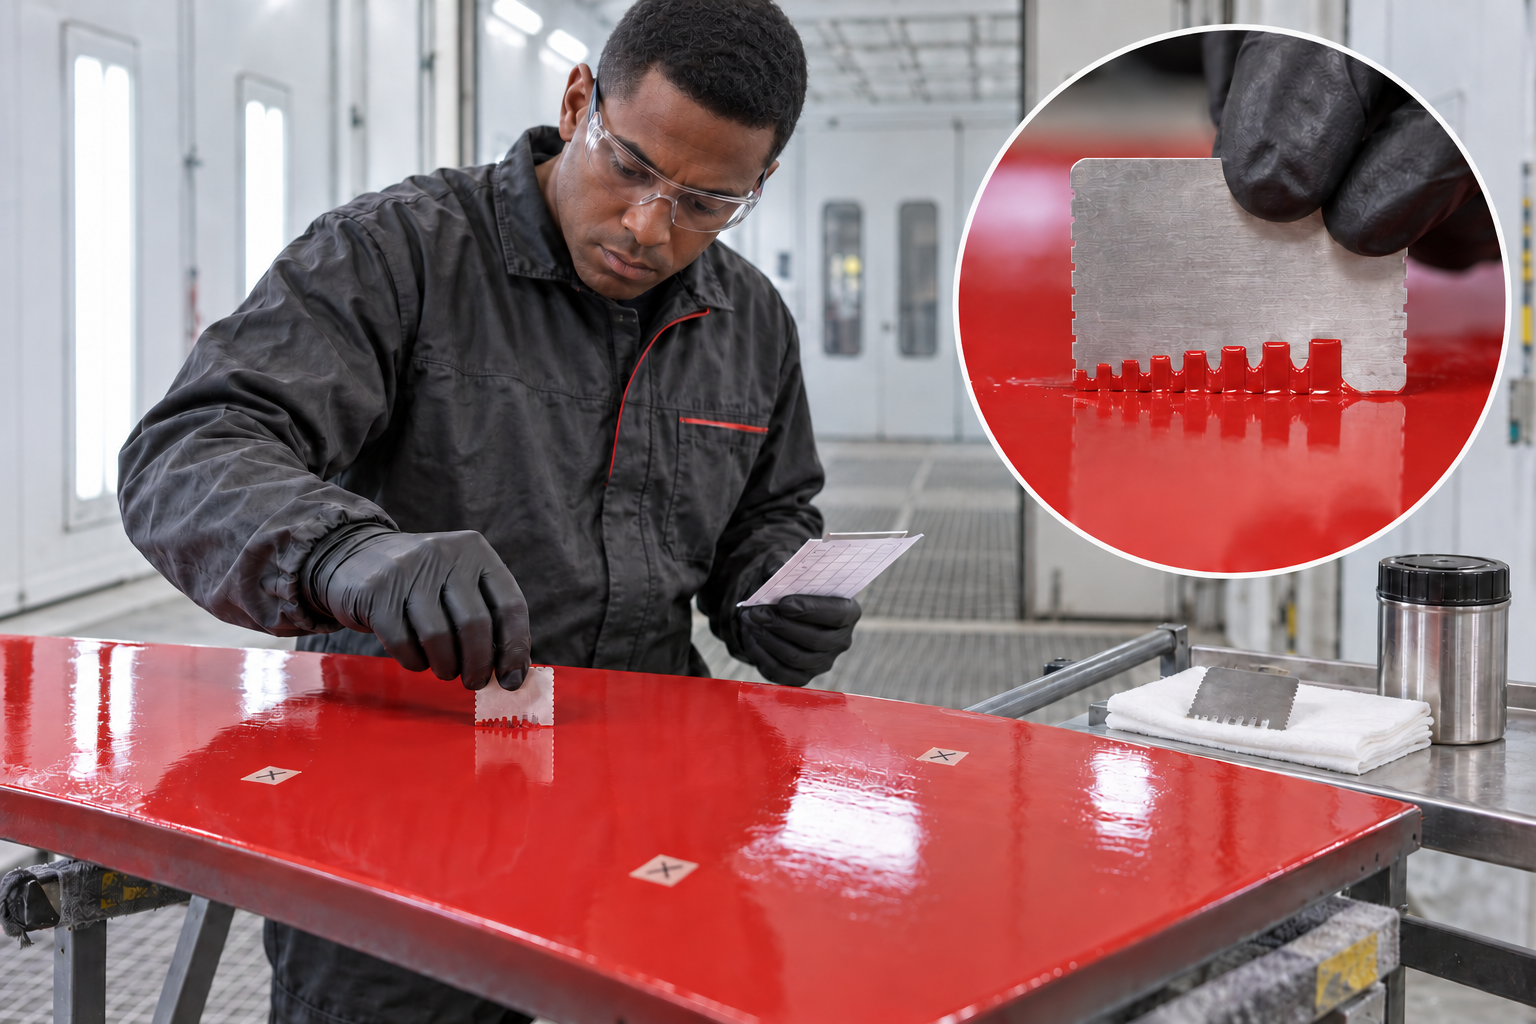
 How to Use a Wet-Film Thickness Gauge
One of the best times to discover that a coating is being applied too thin—or too thick—is while the coating is still wet.
A wet-film thickness gauge gives the applicator immediate information about the amount of coating deposited on the surface. If the wet film is outside the target range, adjustments can often be made before the coating dries and the problem becomes expensive to correct.
This simple tool can help improve coating consistency, reduce rework, control material usage, and increase the likelihood of achieving the specified dry-film thickness.
What Is Wet-Film Thickness?
Wet-film thickness, commonly abbreviated WFT, is the thickness of a liquid coating immediately after application and before its solvent or water evaporates.
Wet-film thickness is commonly measured in:
- Mils: One mil equals one-thousandth of an inch, or 0.001 inch.
- Microns: One micron, also called a micrometer, equals one-millionth of a meter.
One mil equals approximately 25.4 microns.
As a coating dries or cures, volatile ingredients leave the film. The film remaining on the surface is called the dry-film thickness, or DFT. Because of this loss of liquid volume, the final dry film is normally thinner than the original wet film.
What Is a Wet-Film Thickness Gauge?
A wet-film thickness gauge is a flat metal or plastic tool containing a series of calibrated notches or teeth. It may also be called a:
- Wet-film gauge
- Wet-film comb
- Notch gauge
- Step gauge
- WFT gauge
The outside teeth rest on the substrate and establish the reference surface. The progressively shorter inner teeth represent different film-thickness values.
When the gauge is placed into a wet coating, some teeth contact the coating while the higher teeth remain dry. The wet-film thickness lies between the highest wetted tooth and the next higher unwetted tooth.
Why Measure Wet-Film Thickness?
Wet-film measurement is primarily a process-control tool. It tells the applicator what is happening during application, while there may still be time to make corrections.
Checking WFT can help an applicator:
- Apply a more consistent coating film.
- Estimate whether the required DFT will be achieved.
- Detect areas receiving too little material.
- Detect excessive film build before it causes runs or sags.
- Adjust spray-gun speed, distance, overlap, or fluid delivery.
- Control coating consumption.
- Reduce the risk of rework after the coating cures.
- Document the application process.
A coating that is too thin may not provide the expected hiding, barrier protection, chemical resistance, or corrosion resistance. A coating that is too thick may sag, wrinkle, crack, solvent-pop, cure slowly, or trap solvent.
Determine the Target WFT Before Application
Before using the gauge, determine the wet-film thickness needed to produce the specified dry-film thickness.
You will normally need two pieces of information:
- The required dry-film thickness.
- The coating’s percentage of solids by volume.
This information is generally found in the coating manufacturer’s current product data sheet or technical data sheet.
Use solids by volume, not solids by weight. Solids by weight measures mass and should not be substituted in the WFT calculation.
Basic Wet-Film Thickness Formula
For a coating applied without thinner or reducer, use:
Required WFT = Required DFT ÷ Solids by Volume as a Decimal
Example: Coating Applied Without Thinner
Suppose a coating must produce a dry-film thickness of 4 mils and contains 50% solids by volume.
4 mils ÷ 0.50 = 8 mils WFT
The theoretical target is therefore 8 mils wet.
Accounting for Added Thinner or Reducer
Thinner normally adds liquid volume without adding film-forming solids. If the coating is reduced, a greater wet-film thickness will generally be required to produce the same dry-film thickness.
When the percentage of thinner is based on the original coating volume, the following formula may be used:
Required WFT = Required DFT × (1 + Thinner Fraction) ÷ Solids by Volume as a Decimal
Example: Coating Reduced 10%
Assume the same coating requires 4 mils DFT, contains 50% solids by volume, and is reduced 10%.
4 × 1.10 ÷ 0.50 = 8.8 mils WFT
The theoretical wet-film target increases from 8 mils to approximately 8.8 mils.
Do not automatically add thinner merely to change the WFT. Only use a reducer approved by the coating manufacturer and remain within the manufacturer’s permitted reduction range.
How to Use a Wet-Film Thickness Gauge
Step 1: Select the Correct Gauge Range
Choose a gauge that includes the expected wet-film thickness. A gauge with notches close to the target value will provide a more useful reading than one with large intervals between teeth.
Confirm whether the gauge is marked in mils, microns, or both. Do not confuse the two units.
Step 2: Inspect the Gauge
Before taking a reading, make sure the gauge is:
- Clean and free of dried coating.
- Flat and undamaged.
- Easy to read.
- Suitable for the expected thickness range.
Dried coating on the teeth can change their effective depth and produce an inaccurate result.
Step 3: Apply the Coating
Apply the coating using the approved spray, roller, brush, or other application procedure.
The gauge should be used as soon as practical after application. Fast-drying or high-solids materials may begin leveling, setting, skinning, or losing solvent quickly, which can affect the reading.
Step 4: Choose a Representative Test Location
Select a freshly coated area that represents the application being evaluated. When possible, avoid:
- Edges and corners
- Welds and irregular surfaces
- Runs, sags, or visible accumulations
- Areas where the gauge cannot sit squarely
- Previously tested or disturbed areas
Edges, corners, welds, recesses, and complex shapes may require separate evaluation because their film build can differ from broad, flat areas.
Step 5: Place the Gauge Into the Wet Coating
Hold the gauge perpendicular to the coated surface. Press it squarely and firmly into the wet coating until the two outside reference teeth contact the substrate.
Do not slide, twist, drag, or rock the gauge. Movement can displace coating and produce a misleading reading.
Step 6: Remove the Gauge
Lift the gauge straight away from the surface. Remove it perpendicular to the coating rather than dragging it sideways.
Examine the teeth immediately, before the coating begins to flow or dry on the gauge.
Step 7: Read the Gauge
Find:
- The highest-value tooth that is wetted by the coating.
- The next higher-value tooth that remains unwetted.
The wet-film thickness lies between those two values.
Reading Example
If the 8-mil tooth is wet and the 10-mil tooth is dry, the coating’s wet-film thickness is between 8 and 10 mils.
Do not report the reading as exactly 9 mils unless another suitable measuring method supports that conclusion. A notched gauge normally establishes a range bounded by two teeth.
Step 8: Take Additional Readings
One reading represents only one small location. Take readings at multiple representative areas to evaluate application consistency.
The required number and location of readings should come from the project specification, inspection plan, manufacturer’s instructions, or approved quality-control procedure.
Step 9: Clean the Gauge Immediately
Clean reusable gauges before the coating dries. Use only a cleaning material or solvent compatible with the gauge and coating, and follow applicable safety instructions.
Do not scrape, grind, file, or aggressively abrade calibrated teeth. Altering a tooth can permanently affect future readings.
Where Should the Gauge Be Placed?
On a flat surface, place the gauge where its reference teeth can make firm contact with the substrate.
On a cylindrical or curved surface, position the gauge so the reference teeth make stable contact. When practical, take the measurement along the length of the curve rather than across a tight radius.
Small pipes, complex shapes, sharp curves, rough substrates, and heavily profiled steel may prevent the gauge from seating correctly. The limitations of the measurement should be documented.
Common Wet-Film Gauge Mistakes
Using Solids by Weight
The WFT calculation requires solids by volume. Substituting solids by weight can produce a substantially incorrect target.
Ignoring Added Thinner
Reducer increases the liquid volume without normally increasing the volume of film-forming solids. If reduction is ignored, the final dry film may be thinner than expected.
Waiting Too Long to Measure
A wet-film reading should be taken promptly. Solvent evaporation, water loss, absorption, skinning, and leveling can begin almost immediately.
Dragging or Rocking the Gauge
The gauge should be pressed straight into the coating and removed straight out. Dragging or rocking it moves material and can create a false reading.
Reading the Wrong Teeth
The result lies between the highest wetted tooth and the next higher unwetted tooth. It is not based on the first wet tooth encountered when reading the scale in the wrong direction.
Using a Dirty or Damaged Gauge
Dried coating, bent edges, worn markings, or damaged teeth can make the gauge unreliable.
Testing Only One Location
Spray technique, overlap, surface geometry, wind, access, and lighting can create significant variation. One reading cannot represent an entire wall, tank, beam, or production run.
Treating WFT as the Final Acceptance Measurement
Wet-film thickness predicts the likely dry-film build. It does not replace final DFT measurement when dry-film thickness is specified.
What If the Wet Film Is Too Thin?
If readings consistently fall below the target, possible adjustments may include:
- Reducing applicator travel speed.
- Improving spray-pattern overlap.
- Adjusting fluid delivery within equipment and coating limitations.
- Correcting excessive spray distance.
- Applying an additional pass while permitted by the application procedure.
- Checking whether excessive atomizing pressure is increasing overspray.
- Confirming that the material was mixed and reduced correctly.
Do not make uncontrolled equipment or formulation changes. Adjustments must remain within the coating manufacturer’s instructions and the approved application procedure.
What If the Wet Film Is Too Thick?
If readings are above the target, evaluate:
- Applicator travel speed.
- Spray-gun fluid delivery.
- Number of passes.
- Excessive overlap.
- Gun distance and angle.
- Coating viscosity and temperature.
- Accumulation at corners, edges, and welds.
Excessive film build should not be ignored simply because the coating has not sagged. Thick films may develop curing or performance problems that are not immediately visible.
Limitations of Wet-Film Measurement
A notched wet-film gauge provides an approximate thickness range. Several conditions can affect the result:
- Rough or heavily profiled substrates
- Porous or absorbent surfaces
- Uneven coating application
- Fast solvent evaporation
- Rapid curing or skinning
- Coating flow and leveling
- Curved or irregular surfaces
- Incorrect reduction
- Gauge damage or contamination
- Improper placement or reading technique
Surface profile is particularly important on abrasive-blasted steel. The gauge’s reference teeth may contact the peaks of the profile while coating fills the valleys. The resulting reading should be understood as a field-control measurement rather than an exact prediction of the final thickness above every point on the surface.
WFT Is Process Control; DFT Is Final Verification
Wet-film and dry-film measurements answer different questions:
- WFT asks: Are we applying approximately the correct amount of wet coating right now?
- DFT asks: After drying or curing, does the completed coating meet the specified thickness requirements?
For critical protective-coating work, WFT measurements should be followed by appropriate DFT measurements after the coating has dried or cured sufficiently.
Documenting Wet-Film Thickness
A useful field record may include:
- Project and coated-area identification
- Date and time
- Coating manufacturer and product
- Batch or lot number
- Specified DFT range
- Solids by volume
- Amount of thinner or reducer added
- Calculated target WFT
- Gauge range and units
- Individual readings and locations
- Application method
- Ambient and surface conditions
- Adjustments made after testing
- Name of the applicator or inspector
Documentation turns a quick gauge check into useful quality-control information. It can also help explain later DFT results or identify variations in application technique.
Referenced Test Method
The recognized ASTM practice for this measurement is
ASTM D4414—Standard Practice for Measurement of Wet Film Thickness by Notch Gages
.
ASTM standards are copyrighted documents and may be revised. The official current standard should be obtained and followed whenever ASTM D4414 is required by a contract, specification, inspection plan, or quality-control procedure.
The Bottom Line
A wet-film thickness gauge is inexpensive, portable, and easy to use—but only when the applicator understands what the reading means.
Calculate the target using solids by volume. Account for approved thinner. Measure immediately. Press the gauge squarely into the coating. Read between the highest wetted tooth and the next higher unwetted tooth. Take multiple readings, clean the gauge, and verify the completed work with dry-film measurements when required.
Thirty seconds spent checking the wet film can prevent hours of sanding, recoating, explaining, and repairing after the coating cures.
Technical Notice: This article provides general educational information and does not replace the coating manufacturer’s instructions, project specification, safety requirements, or complete ASTM test method. Always use the current product data sheet and the current edition of the specified standard. Testing and application should be performed by appropriately trained personnel.
Copyright © 2026 Azimuth Spray Systems, LLC. All rights reserved. AirSprayTech.com—The Finishing Authority®. No portion of this article may be reproduced, distributed, republished, or transmitted without prior written permission.