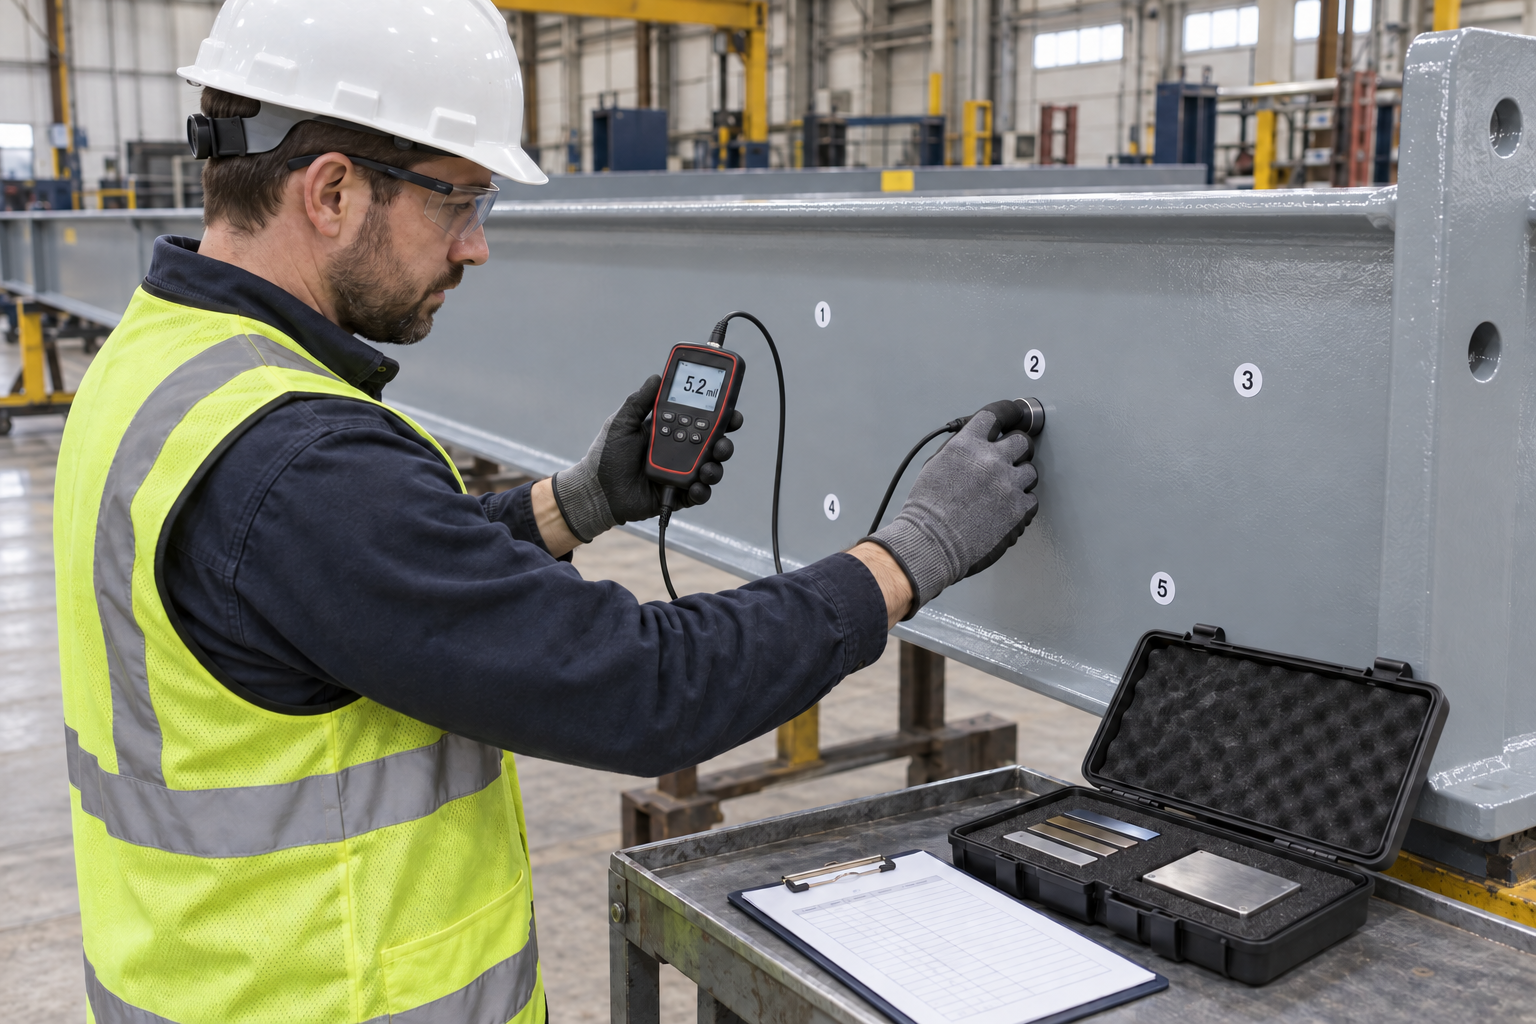
 How to Measure Dry-Film Thickness
A coating can look uniform and still be too thin to provide the expected protection—or so thick that it develops curing and performance problems. Dry-film thickness measurement provides objective information about how much coating remains on the surface after drying or curing.
Dry-film thickness, commonly abbreviated DFT, is one of the most frequently specified and measured properties of an applied coating. It affects hiding, adhesion, flexibility, hardness, corrosion protection, chemical resistance, appearance, and service life.
Measuring DFT correctly requires more than placing a probe on the surface and recording the number displayed. The inspector must select the correct instrument, verify its accuracy, account for the substrate and surface profile, collect enough readings, and evaluate the results according to the project specification.
What Is Dry-Film Thickness?
Dry-film thickness is the thickness of a coating remaining on the substrate after the material has dried or cured sufficiently for measurement.
DFT may refer to:
- The thickness of one individual coat.
- The combined thickness of several coats.
- The total thickness of the complete coating system.
Most conventional magnetic and eddy-current gauges measure the total thickness between the probe and the underlying metal. They generally do not identify the thickness of each individual layer in a multicoat system.
Common Units of Measurement
Dry-film thickness is commonly reported in:
- Mils: One mil equals 0.001 inch.
- Microns: One micron, or micrometer, equals one-millionth of a meter.
One mil equals approximately 25.4 microns.
Always confirm which unit is required. Confusing mils with millimeters—or recording microns as mils—can produce a serious reporting error.
Why Is Dry-Film Thickness Important?
Coatings are formulated to perform within an intended thickness range. Applying more or less material than specified can change the way the coating dries, cures, adheres, and performs.
When the Coating Is Too Thin
Insufficient DFT may contribute to:
- Poor hiding or uneven color.
- Reduced barrier protection.
- Premature corrosion.
- Pinholes or incomplete coverage.
- Reduced chemical or moisture resistance.
- Shortened coating service life.
- Failure to meet the project specification.
When the Coating Is Too Thick
Excessive DFT may contribute to:
- Slow or incomplete cure.
- Solvent entrapment.
- Wrinkling or mud cracking.
- Sagging or excessive edge buildup.
- Loss of flexibility.
- Cracking or delamination.
- Excessive material consumption.
- Problems applying the next coat.
More coating is not automatically better. The correct amount of coating is better.
What Type of DFT Gauge Is Required?
The correct gauge depends primarily on the substrate beneath the coating. A gauge designed for steel may not work on aluminum, and a conventional metal-substrate gauge will not measure a coating on wood or concrete.
Magnetic Gauges for Ferrous Metal
Magnetic instruments measure nonmagnetic coatings applied over ferrous substrates such as carbon steel and iron.
These gauges may be used for coatings such as:
- Paint over carbon steel
- Epoxy over steel
- Polyurethane over steel
- Powder coating over steel
- Nonmagnetic linings over steel
Some mechanical magnetic pull-off gauges use the force required to pull a magnet from the coated surface. Electronic magnetic gauges use changes in magnetic properties to calculate the distance between the probe and the metal.
Eddy-Current Gauges for Nonferrous Metal
Eddy-current instruments measure nonconductive coatings applied over electrically conductive nonferrous metals.
Examples include:
- Paint over aluminum
- Powder coating over aluminum
- Coatings over copper
- Coatings over brass
- Nonconductive finishes over certain stainless steels
The substrate must be electrically conductive, and the coating must be sufficiently nonconductive for the selected instrument.
Combination Ferrous and Nonferrous Gauges
Many electronic gauges can automatically determine whether the probe is positioned over a ferrous or nonferrous metal and select the appropriate measurement principle.
Automatic selection is convenient, but the inspector should still know the substrate being measured. Unusual alloys, thin metal, curvature, or mixed-metal assemblies may affect instrument response.
Ultrasonic Gauges for Nonmetallic Substrates
Ultrasonic instruments may be used to measure certain organic coatings applied over:
- Concrete
- Wood
- Plastic
- Fiberglass
- Wallboard
- Composite materials
Ultrasonic gauges send a signal through the coating and measure its reflection from an interface. The coating and substrate must be different enough acoustically for the instrument to recognize the boundary.
Referenced method:
ASTM D6132—Nondestructive Measurement of Dry Film Thickness Using an Ultrasonic Coating Thickness Gauge
.
Not every coating and substrate combination can be measured ultrasonically. Whenever possible, verify performance using a sample of known thickness made from the same coating and substrate.
Can a Gauge Measure Individual Coating Layers?
A conventional magnetic or eddy-current gauge normally reports the total distance between the probe and the metal substrate. If a steel surface has a primer, intermediate coat, and topcoat, the instrument will generally report their combined thickness.
Individual layers can sometimes be determined by:
- Measuring and documenting each coat before applying the next.
- Using a destructive cross-sectional thickness gauge.
- Using specialized ultrasonic equipment capable of identifying separate interfaces.
- Preparing companion test panels with the same coating system.
The ability to display several layers should never be assumed. Confirm the capability with the instrument manufacturer and verify it on a representative coating system.
Calibration, Verification, and Adjustment Are Different
These three terms are often used as if they mean the same thing. In coating inspection, they describe different activities.
Calibration
Calibration is a controlled, documented process performed over the operating range of the instrument using traceable standards. It is normally performed by the equipment manufacturer, an authorized agent, or an appropriately accredited calibration laboratory.
Pressing the zero button at the jobsite is not the same as calibrating the instrument.
Verification of Accuracy
Verification confirms that the gauge is reading within its allowable tolerance. It is performed using certified coated standards or certified shims appropriate for the gauge and anticipated measurement range.
Gauge accuracy should be verified according to the governing standard, project requirements, and manufacturer’s instructions. It should also be rechecked if the instrument is dropped, damaged, producing questionable readings, or subjected to conditions that may affect its operation.
Adjustment
Adjustment aligns the gauge to the characteristics of the surface being measured. These characteristics may include:
- Surface roughness
- Metal composition
- Curvature
- Part thickness
- Part geometry
An adjustment made for one surface may not remain valid when the substrate, curvature, profile, alloy, or geometry changes.
A helpful technical discussion of these distinctions is available from
DeFelsko: Calibration, Verification, and Adjustment
.
How to Measure Dry-Film Thickness
Step 1: Review the Specification
Before taking readings, determine:
- The specified minimum and maximum DFT.
- Whether the requirement applies to each coat or the total system.
- The required test method.
- The required number and location of measurements.
- Whether localized high or low readings are permitted.
- How spot measurements and area measurements are calculated.
- Whether different thickness-restriction levels apply.
- How nonconforming areas are identified and corrected.
The coating manufacturer’s product data sheet may provide a recommended range, while the project specification may establish a different contractual requirement. Questions should be resolved before acceptance testing begins.
Step 2: Confirm That the Coating Is Ready
The coating must be sufficiently dry or cured to withstand contact with the probe.
Placing a probe on a soft film can:
- Indent the coating.
- Produce a falsely low reading.
- Contaminate the probe.
- Damage the appearance of the finish.
Follow the coating manufacturer’s instructions regarding dry time, cure time, recoat time, and handling.
Step 3: Identify the Substrate
Determine whether the coating is applied over ferrous metal, nonferrous metal, concrete, wood, plastic, or another material.
Do not identify the substrate based only on appearance. Galvanized steel, aluminum, stainless steel, and painted carbon steel can resemble one another while requiring different measurement considerations.
Step 4: Select the Correct Probe and Range
Choose a gauge and probe suitable for:
- The substrate.
- The expected coating thickness.
- The surface temperature.
- The size and shape of the part.
- The degree of curvature.
- The roughness of the surface.
- The size of the available measurement area.
A general-purpose probe may work well on a broad, flat surface but poorly on a small pipe, narrow flange, bolt head, edge, or inside corner.
Step 5: Inspect the Gauge and Probe
Before use, check for:
- Damage to the probe tip.
- Paint, metal particles, dust, or debris on the probe.
- Damage to the probe cable.
- Low battery condition.
- Loose connections.
- Incorrect measurement units.
- An adjustment remaining from a previous project.
Clean the probe according to the manufacturer’s instructions. Do not grind or aggressively abrade the measuring surface.
Step 6: Confirm Calibration Status
Confirm that the gauge has a current calibration status acceptable to the project specification or quality program.
A certificate of calibration should identify the instrument, calibration provider, traceability, date, procedure, and calibration results. A certificate of conformance is not necessarily the same as a documented certificate of calibration.
Step 7: Verify Gauge Accuracy
Verify the gauge using appropriate certified reference standards or shims. The verification thickness should be within or near the expected measurement range whenever practical.
Follow the gauge manufacturer’s instructions and account for the stated tolerances of both the gauge and the reference standard.
If the gauge does not read within the permitted tolerance, do not simply continue measuring. Determine whether the gauge, probe, standard, adjustment, or technique is responsible.
Step 8: Check the Uncoated Substrate
Whenever possible, measure an uncoated area of the same substrate. This helps identify the effects of:
- Surface profile
- Curvature
- Metal composition
- Part thickness
- Edge geometry
- Residual magnetism
The most representative adjustment is normally made on the actual uncoated substrate—or an uncoated reference sample with the same material, geometry, and surface preparation.
Step 9: Adjust the Gauge When Required
Follow the manufacturer’s instructions and specified test method to adjust the gauge for the surface being measured.
On smooth metal, this may involve a zero adjustment or measuring certified shims placed on the uncoated substrate.
On abrasive-blasted steel, the surface profile must be considered. A simple zero adjustment performed directly on a rough surface may not produce the required measurement above the profile peaks. The specified standard and gauge instructions should determine the correction or adjustment procedure.
Step 10: Clean the Test Area
The coating surface should be free from:
- Dirt
- Dust
- Loose overspray
- Moisture
- Metal particles
- Uncured residue
- Other material that could separate the probe from the coating
Do not damage or polish the coating while cleaning the test area.
Step 11: Position the Probe Correctly
Place the probe flat and perpendicular to the coated surface. Lower it carefully and allow the instrument to take the reading.
Do not:
- Drag the probe across the coating.
- Rock or tilt the probe.
- Press excessively into a soft film.
- Allow the probe to overhang an edge.
- Take readings on loose contamination.
Lift the probe clear of the surface between readings unless the instrument is specifically designed for continuous scanning.
Step 12: Take Multiple Gauge Readings
One gauge reading represents one very small point. Coating thickness naturally varies because of:
- Surface profile.
- Spray-pattern distribution.
- Applicator technique.
- Gun angle and distance.
- Overlap.
- Part geometry.
- Edges, welds, corners, and recesses.
- Coating flow and leveling.
Collect multiple readings in the defined measurement area. Evaluate them according to the sampling and averaging procedure required by the specification.
Under SSPC-PA 2 terminology, an individual instrument result is a gauge reading. Multiple gauge readings are used to produce spot measurements, which are then used to determine conformance within a larger inspection area.
Step 13: Investigate Unusual Readings
Do not automatically delete a reading merely because it is higher or lower than expected. First determine whether it represents:
- An actual thin or thick area.
- A surface irregularity.
- Contamination on the coating or probe.
- Incorrect probe position.
- An edge or curvature effect.
- A weld or localized buildup.
- An instrument or adjustment problem.
Repeat the reading nearby and document confirmed nonconforming areas.
Step 14: Recheck Gauge Accuracy
Recheck the gauge against the reference standard at the frequency required by the project, manufacturer, or quality procedure.
Accuracy should also be rechecked if:
- The gauge is dropped.
- The probe is damaged.
- Readings become erratic.
- The substrate or geometry changes.
- A large number of readings has been collected.
- Environmental conditions change substantially.
If the final verification is unacceptable, measurements taken since the last successful verification may need to be evaluated again.
Understanding Surface-Profile Effects
Abrasive blasting creates a surface profile composed of peaks and valleys. The applied coating fills the valleys and covers the peaks.
A magnetic gauge does not physically locate the top of every profile peak. It responds to a magnetic plane within the roughened steel. Without an appropriate adjustment or correction, the instrument may report a thickness that includes part of the profile effect.
Surface-profile influence depends on:
- Profile depth and shape.
- Probe design.
- Gauge type.
- Coating thickness.
- Steel properties.
- The adjustment or correction method.
For protective coatings over blast-cleaned steel, follow the project-specified procedure rather than applying an improvised correction.
International guidance for rough steel surfaces is available in
ISO 19840—Measurement and Acceptance Criteria for Dry-Film Thickness on Rough Surfaces
.
Measurements Near Edges, Corners, and Welds
Edges, corners, welds, bolts, small-diameter pipe, and narrow flanges can be difficult to measure accurately.
Potential problems include:
- The probe overhanging the edge.
- Insufficient flat area for the probe.
- Changes in metal mass or geometry.
- Heavy coating accumulation near welds.
- Thin films on sharp edges.
- Inability to position the probe perpendicular to the surface.
A small or specialized probe may be needed. Verify the probe’s performance on an uncoated surface or representative sample with similar geometry.
Measuring Coatings Over Galvanized Steel
Paint applied over galvanized steel creates a duplex coating system consisting of paint over a zinc layer over steel.
A conventional magnetic gauge may report the combined thickness of the paint and zinc because both separate the probe from the ferrous steel substrate. It may not report the paint layer alone.
Determining the individual paint and zinc thicknesses may require:
- Measurements of the galvanizing before painting.
- A specialized duplex-coating probe.
- A destructive cross-sectional method.
- Another approved analytical procedure.
Do not assume that a total reading represents only the paint.
Measuring Coatings Over Stainless Steel
Stainless steel cannot be treated as one uniform substrate category. Some stainless steels are sufficiently magnetic for a magnetic gauge, while others may be measured using an eddy-current principle. Forming, welding, composition, and heat treatment can affect magnetic properties.
Verify gauge operation on an uncoated area of the actual stainless-steel substrate or a representative sample before accepting measurements.
Temperature and Environmental Effects
Gauges and probes have operating-temperature limitations. Hot surfaces can affect instrument accuracy, damage the probe, or shorten probe life.
Cold instruments brought into a warm, humid environment may develop condensation. Strong magnetic fields, residual magnetism, and certain electrical equipment may also affect some gauges.
Allow equipment to stabilize when environmental conditions change and follow the manufacturer’s operating limits.
Common DFT Measurement Mistakes
Calling a Field Adjustment “Calibration”
Zeroing or adjusting a gauge at the jobsite is not the same as a controlled calibration performed by the manufacturer or qualified laboratory.
Using the Wrong Gauge for the Substrate
A magnetic gauge intended for carbon steel will not automatically measure paint over aluminum, concrete, wood, or plastic.
Failing to Verify Accuracy
A calibration certificate does not guarantee that the gauge remains accurate after transportation, use, contamination, wear, or accidental damage.
Ignoring Surface Profile
Abrasive-blasted steel can produce a positive measurement bias if profile effects are not addressed according to the required procedure.
Taking Only One Reading
Coating thickness varies. A single reading is not normally sufficient to characterize a spot, component, or inspection area.
Tilting or Dragging the Probe
Improper probe position can affect the reading and damage the probe tip.
Measuring Too Close to an Edge
If the probe overhangs or cannot sit flat, the reading may be unreliable.
Measuring a Soft Coating
The probe may compress or indent an incompletely cured film and produce a falsely low result.
Confusing Total System Thickness With Individual-Coat Thickness
Most conventional gauges measure all nonmagnetic or nonconductive layers between the probe and the metal substrate.
Averaging Away a Defect
Averages are useful, but they should not be used to conceal confirmed localized thin spots when the specification restricts individual or localized measurements.
How Many Measurements Are Required?
There is no universal number that applies to every coating project. Measurement frequency depends on:
- The governing standard.
- The project specification.
- The size and configuration of the coated area.
- The type of structure.
- The coating system.
- The required confidence level.
- Observed application consistency.
SSPC-PA 2 is frequently specified for determining conformance on coated metal structures. It establishes procedures for collecting readings, calculating spot measurements, defining test areas, and evaluating thickness restrictions.
Referenced standard:
SSPC-PA 2—Procedure for Determining Conformance to Dry Coating Thickness Requirements
.
The complete current standard should be consulted rather than relying on a simplified summary.
A Test Method Is Not an Acceptance Standard
This distinction matters.
ASTM D7091 explains how nondestructive DFT measurements are obtained using magnetic and eddy-current gauges. SSPC-PA 2 provides a procedure for determining whether collected measurements conform to specified thickness requirements.
Neither document independently determines the correct thickness for every coating. The required DFT must come from the project specification, manufacturer’s instructions, contract documents, or other governing requirement.
What Should Be Recorded?
A useful DFT inspection record may include:
- Project name and location
- Date and time
- Coated component or area
- Coating manufacturer and product
- Batch or lot number
- Coating system and number of coats
- Specified DFT range
- Substrate type
- Surface-preparation method and profile
- Gauge manufacturer and model
- Gauge and probe serial numbers
- Measurement units
- Calibration status
- Reference standards used for verification
- Gauge adjustment or correction method
- Individual gauge readings
- Calculated spot and area measurements
- Location of measurements
- Nonconforming areas
- Corrective action and retest results
- Name of the inspector or technician
Primary Referenced Standards
The Bottom Line
Measuring dry-film thickness is not difficult, but obtaining a defensible result requires more than turning on a gauge.
Identify the substrate. Select the correct probe. Confirm calibration status. Verify accuracy. Adjust for the actual surface when required. Position the probe correctly. Take multiple readings. Evaluate them according to the specified procedure. Document what was measured and how the final determination was made.
The gauge supplies the readings. The test method organizes those readings. The project specification determines whether the coating passes or fails.
Technical Notice: This article provides general educational information and does not reproduce or replace the complete ASTM, AMPP/SSPC, ISO, coating-manufacturer, instrument-manufacturer, contract, or project requirements. Standards are revised periodically. Always obtain and follow the current edition of the specified method. Coating inspection should be performed by appropriately trained personnel using suitable equipment and established acceptance criteria.
Copyright © 2026 Azimuth Spray Systems, LLC. All rights reserved. AirSprayTech.com—The Finishing Authority®. No portion of this article may be reproduced, distributed, republished, or transmitted without prior written permission.