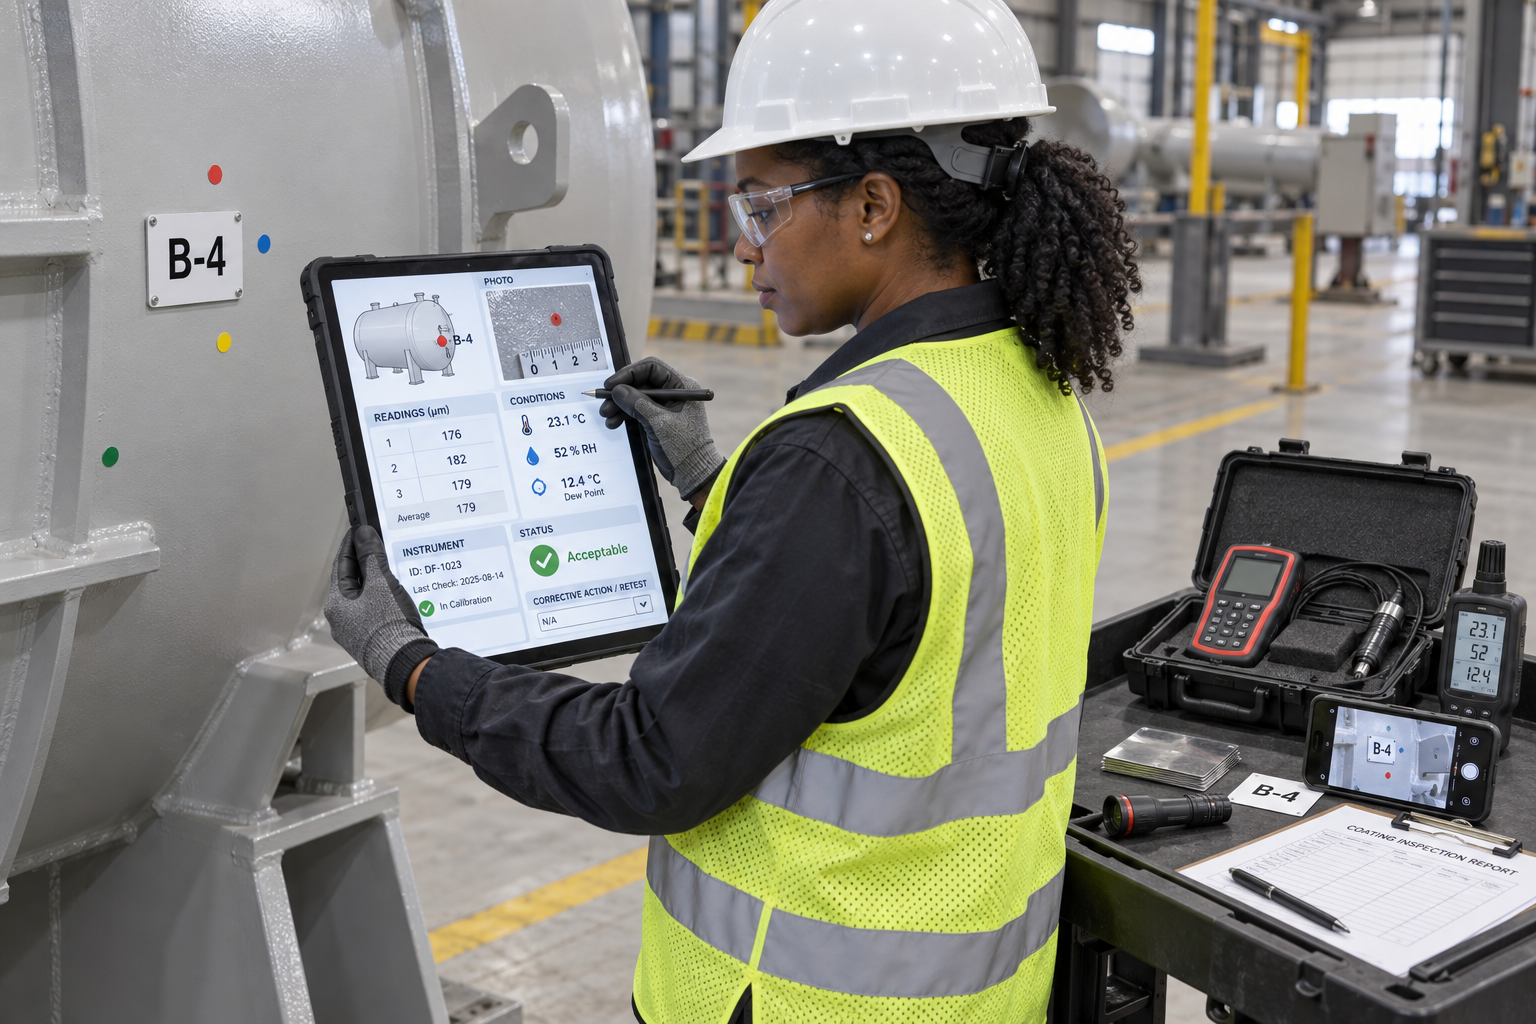
 If It Isn’t Written Down, It Didn’t Happen: How to Document a Coating Inspection
A coating inspection is not complete when the measurements are taken. It is complete when another qualified person can review the records and understand what was inspected, where it was inspected, how it was tested, what equipment was used, and whether the work met the project requirements.
Good documentation creates a permanent record of the coating work. It can support progress payments, warranty claims, maintenance planning, quality-control decisions, and the investigation of a future coating failure.
A few photographs and a note saying “paint looks good” are not an inspection report. Professional coating documentation must be organized, objective, traceable, and supported by measurements.
Why Coating Inspection Documentation Matters
A protective coating may remain in service for many years. The people who applied and inspected it may no longer be available when a problem develops. The inspection report may become the only reliable record of the original work.
Complete documentation helps establish:
- Which surfaces were inspected
- What coating materials were applied
- How the surface was prepared
- Whether environmental conditions were acceptable
- Whether specified wet- and dry-film thicknesses were achieved
- Whether defects, contamination, or application problems were observed
- What tests were performed and which standards were followed
- What corrective work was required and completed
- Whether the completed work met the project specification
ASTM D3276, Standard Guide for Painting Inspectors (Metal Substrates), provides guidance concerning the inspection of coating work on metal substrates. AMPP also offers guidance through its Guide for Planning Coatings Inspection.
Documentation Begins Before Work Starts
The inspector should not wait until coating application begins to decide what information to record. Documentation requirements should be established during pre-job planning.
Before the work begins, review:
- The coating specification
- Approved product data sheets
- Safety data sheets
- Coating manufacturer’s written instructions
- Approved coating-system schedule
- Surface-preparation requirements
- Required inspection and test methods
- Acceptance criteria
- Inspection frequency and sampling plan
- Hold points and witness points
- Repair procedures
- Required report forms
- Distribution and retention requirements for inspection records
The inspector should also understand the limits of the assigned authority. The specification or inspection plan should identify who can stop work, reject work, approve repairs, change acceptance criteria, or authorize deviations.
What Is a Hold Point?
A hold point is a stage of the work that cannot proceed until a required inspection has been completed and approval has been given. Examples may include:
- Approval of the prepared surface before primer application
- Inspection of stripe coating before the full coat is applied
- Acceptance of primer thickness before an intermediate coat
- Holiday testing before equipment is placed into service
- Final inspection before scaffolding or containment is removed
A witness point normally gives an identified party the opportunity to observe an inspection or operation. The project documents should define exactly how hold points and witness points are handled.
The Daily Coating Inspection Report
The daily report is the foundation of coating documentation. It should be completed during the work—not reconstructed from memory several days later.
Each daily report should normally include the following information.
1. Project Identification
- Project name and number
- Owner or facility
- Contractor and subcontractor
- Inspector’s name and employer
- Report number
- Date and work shift
- Specific structure, component, room, elevation, or work area
Use consistent location descriptions. “North wall, Grid B-4, elevation 12 to 20 feet” is more useful than “wall near the door.” Equipment numbers, drawing references, grid coordinates, tank course numbers, column lines, or marked-up plans can make inspection locations traceable.
2. Personnel and Work Activities
Record the contractor’s supervisor, coating applicators, abrasive blasters, and other relevant personnel working in the inspection area. Briefly describe the work performed during the shift, including:
- Containment setup
- Cleaning and degreasing
- Abrasive blasting or power-tool cleaning
- Stripe coating
- Primer, intermediate, or topcoat application
- Touch-up and repair work
- Testing and final inspection
The report should distinguish between work observed by the inspector and work reported by someone else.
3. Weather and Environmental Conditions
Environmental conditions can determine whether a coating cures properly or fails prematurely. At the required intervals, document:
- Air temperature
- Surface temperature
- Relative humidity
- Dew-point temperature
- Difference between surface temperature and dew point
- Wind, rain, condensation, direct sunlight, or changing weather
- Conditions inside the containment or enclosed work area
Record the time and exact location of each set of readings. Environmental readings taken on a shaded north-facing surface may not represent a steel surface heated by direct sunlight.
ASTM E337 addresses humidity measurement using psychrometers. The coating manufacturer’s product data sheet and project specification should determine the allowable environmental limits.
4. Inspection Equipment
Identify the equipment used to make acceptance decisions. Depending on the work, this may include:
- Dry-film thickness gauge
- Wet-film thickness gauge
- Surface-profile gauge or replica tape
- Psychrometer or electronic environmental meter
- Surface thermometer
- Soluble-salt test equipment
- Holiday detector
- Adhesion tester
- Low-voltage lighting or inspection mirror
- Conductivity meter
For critical instruments, record:
- Equipment type
- Manufacturer
- Model
- Serial number or unique identification number
- Calibration or certification status
- Reference standards used for verification
- Pre-use and post-use verification results
Do not use the terms calibration, verification of accuracy, and adjustment interchangeably. Record what was actually done, using the terminology of the applicable standard and instrument manufacturer.
5. Coating Materials
Every coating material should be traceable. Record:
- Manufacturer
- Product name and product number
- Color
- Batch or lot numbers
- Component numbers
- Manufacturing or expiration dates when applicable
- Thinner or reducer used
- Quantity of thinner added
- Mixing ratio
- Induction time
- Pot life
- Material temperature when required
- Storage conditions
When plural-component material is used, record the identification of both components. If several batches are used in one work area, document where each batch was applied whenever practical.
6. Surface Condition Before Preparation
Record the condition of the substrate and existing coating before work begins. Note:
- Rust and corrosion
- Mill scale
- Oil and grease
- Dirt and dust
- Soluble salts
- Existing coating condition
- Weld spatter and sharp edges
- Laminations, pits, cracks, or other substrate defects
- Moisture or condensation
- Previous repairs
Photograph significant conditions before they are changed or covered.
7. Surface Preparation
Document the preparation method and the resulting surface condition. The report may include:
- Specified and achieved degree of cleanliness
- Abrasive type, size, manufacturer, and lot
- Abrasive cleanliness
- Surface-profile readings
- Dust level
- Soluble-salt test results
- Condition of compressed air
- Power tools or blast equipment used
- Areas requiring additional preparation
- Time between preparation and priming
ASTM D4417 covers field measurement of surface profile on blast-cleaned steel. ASTM D4285 addresses the indication of oil or water in compressed air.
8. Coating Application
Record how each coat was applied and identify the equipment used. Include:
- Coat number and type
- Start and completion times
- Application method
- Spray-equipment type
- Tip or nozzle size when relevant
- Material and ambient temperatures
- Stripe-coat locations
- Areas masked or excluded
- Wet-film thickness readings
- Observed application problems
- Interruptions or changes in conditions
ASTM D4414 describes the use of a notch gauge for measuring wet-film thickness. Wet-film readings help the applicator make corrections while the coating is still wet.
9. Dry-Film Thickness
Dry-film thickness documentation should show more than a single average. Record:
- Inspection area or measurement location
- Individual gauge readings when required
- Spot measurements
- Area averages
- Lowest and highest readings
- Specified minimum and maximum thickness
- Number of readings taken
- Areas below or above the permitted range
- Corrective action and retest results
For measurement of dry-film thickness on metal substrates, consult ASTM D7091 and the measurement procedure specified by the project. On abrasive-blasted steel, the effect of surface profile must be handled in accordance with the governing standard or specification.
Do not average unacceptable areas into compliance. If the specification defines spot measurements, inspection areas, minimums, maximums, or restricted values, report the results in that same format.
10. Cure and Recoat Information
Document the elapsed time between coats and whether the work remained within the manufacturer’s recoat window. Also record:
- Application completion time
- Temperature during cure
- Minimum curing period
- Time of the next coat
- Maximum recoat interval
- Required surface treatment if the interval was exceeded
- Hardness or solvent-resistance results when specified
- Time before handling, immersion, or return to service
If a cure test is required, identify the test method, material tested, location, acceptance criteria, and results. Avoid vague statements such as “paint was dry.” Dry to the touch does not necessarily mean fully cured.
11. Final Appearance and Film Defects
Inspect the completed coating under suitable lighting. Document conditions such as:
- Runs, sags, and curtains
- Pinholes and holidays
- Overspray and dry spray
- Blistering
- Cracking, checking, or flaking
- Wrinkling or lifting
- Uneven color or gloss
- Embedded debris
- Thin areas and misses
- Damage from handling or other trades
ISO 13076 provides guidance concerning lighting and procedures for visual assessment of coatings.
How to Record Test Results
Every recorded test result should answer six questions:
- What was tested?
- Where was it tested?
- When was the test performed?
- How was it tested?
- What was the result?
- Did the result comply with the requirement?
For example, “DFT acceptable” is incomplete. A useful entry would identify the structure, inspection area, coat or coating system, instrument, test procedure, number of measurements, specified range, measured results, and acceptance status.
Photographing a Coating Inspection
Photographs can be powerful evidence, but only when they are identifiable and placed in context.
Use a Three-Photograph Sequence
- Orientation photograph: Shows the structure or general work area.
- Location photograph: Shows where the condition exists on the structure.
- Close-up photograph: Shows the defect, instrument reading, or test area.
Include Scale and Identification
When practical, include a ruler, reference card, test marker, location label, or other known scale. A close-up of a crack without scale may not show whether it is a hairline defect or a large opening.
Record Essential Photograph Information
- Photograph number
- Date and time
- Location
- Direction of view
- Description of what the photograph shows
- Relationship to the inspection report or nonconformance item
Preserve the original image files. Avoid filters, enhancements, or edits that could misrepresent the condition. If arrows or labels are added to a copy, retain the unedited original.
Use Objective Language
An inspection report should state observable facts. Avoid emotional, accusatory, or speculative language.
| Avoid |
Document Instead |
| The blaster did a bad job. |
Visible coating remained on approximately 15% of Area B-4 after preparation. |
| The paint was too thin. |
Three spot measurements were below the specified minimum of 6 mils. |
| The coating was probably mixed wrong. |
The coating remained soft 48 hours after application; mixing records were not available for review. |
| The surface was wet. |
Visible condensation was observed on the west wall at 7:35 a.m.; coating application had not begun. |
Separate observations from conclusions. If the cause of a condition has not been established, describe the condition and identify what additional investigation is needed.
Documenting a Nonconformance
A nonconformance occurs when materials, workmanship, conditions, or test results do not meet a specified requirement.
A nonconformance report should identify:
- The exact location and extent of the condition
- The requirement that was not met
- The measured or observed condition
- The date and time discovered
- Who was notified
- Any immediate action taken
- The proposed corrective action
- Who authorized the repair
- The date the repair was completed
- Retest or reinspection results
- Final disposition and closure approval
Do not erase or rewrite the original result after a repair. Preserve the initial nonconforming result and add the corrective action and retest result. This creates a complete inspection trail.
Documenting Adhesion Tests
An adhesion result is incomplete without the mode and location of failure. For a pull-off test, record:
- Test method
- Tester manufacturer and model
- Dolly size
- Adhesive used
- Surface preparation before bonding
- Adhesive-curing time
- Whether the coating was cut around the dolly
- Loading rate when required
- Maximum pressure or pull-off value
- Percentage and location of adhesive or cohesive failure
- Photographs of the dolly and test surface
ASTM D4541 covers pull-off strength testing with portable adhesion testers. For tape adhesion testing, consult ASTM D3359. The selected test must be appropriate for the coating, substrate, specification, and service conditions.
Documenting Holiday Testing
When holiday detection is required, record:
- Test method and governing standard
- Detector manufacturer, model, and serial number
- Low- or high-voltage test method
- Coating-system thickness
- Test voltage or instrument setting
- Grounding arrangement
- Verification of instrument operation
- Area tested
- Number and location of holidays found
- Repair material and procedure
- Retest results after repair
ASTM D5162 provides practices for holiday testing of nonconductive protective coatings on metallic substrates.
Common Documentation Mistakes
- Using vague or inconsistent location descriptions
- Recording averages without the supporting measurements
- Failing to identify the test instrument
- Omitting batch and lot numbers
- Taking photographs without scale or location information
- Recording environmental conditions only once per shift
- Failing to document work that was rejected or repaired
- Changing an original entry without preserving the correction history
- Using opinion instead of measurable facts
- Failing to identify the standard or procedure followed
- Reporting a test as passed without stating the acceptance criteria
- Waiting until the end of the project to complete daily reports
Correcting an Inspection Record
If a handwritten entry must be corrected, draw a single line through the original information so it remains readable. Add the correct information, the date, and the inspector’s initials. Do not erase, cover, or destroy the original entry.
Electronic systems should preserve an audit trail showing what was changed, when it was changed, and who made the change. Once issued, inspection reports should follow the project’s revision-control procedure.
Building the Final Coating Inspection Report
The final report should organize the project record so that it can be reviewed without searching through disconnected files. Depending on the project, it may include:
- Executive summary
- Project identification and scope
- Applicable specifications and standards
- Approved coating-system information
- Inspector qualifications
- Equipment and calibration records
- Daily inspection reports
- Environmental-condition logs
- Surface-preparation records
- Coating-material and batch records
- Wet- and dry-film thickness results
- Adhesion, cure, holiday, or other test results
- Photographic records
- Nonconformance and corrective-action records
- Punch-list completion
- Final acceptance documentation
A Practical Daily Report Checklist
Before completing the report, confirm that it answers the following questions:
- Can another person identify the exact area inspected?
- Are the date, time, weather, and environmental readings recorded?
- Are the coating product and batch numbers identified?
- Are preparation and application activities described?
- Are measurements connected to specific locations?
- Are the applicable acceptance criteria stated?
- Are inspection instruments traceable?
- Are photographs numbered and described?
- Are rejected areas and corrective actions documented?
- Does the report clearly distinguish facts from conclusions?
- Is the report signed or electronically approved?
Referenced Standards and Resources
The Bottom Line
A good coating inspector does more than take readings. The inspector creates a clear and defensible record of the work.
Document the location, conditions, materials, equipment, methods, results, acceptance criteria, defects, repairs, and final disposition. Write objectively, preserve original records, and make every photograph and measurement traceable.
The coating may eventually be covered, placed into service, or exposed to years of weathering. A well-prepared inspection report preserves the story of how that coating system was installed—and provides the evidence needed if questions arise later.
Technical Notice: This article provides general educational information and does not replace a project specification, qualified coating inspector, coating manufacturer’s instructions, or the complete requirements of an applicable standard. Always consult the current edition of the specified inspection and test methods.
Copyright © 2026 Azimuth Spray Systems, LLC. All rights reserved. AirSprayTech.com—The Finishing Authority®. No portion of this article may be reproduced, distributed, or republished without prior written permission.